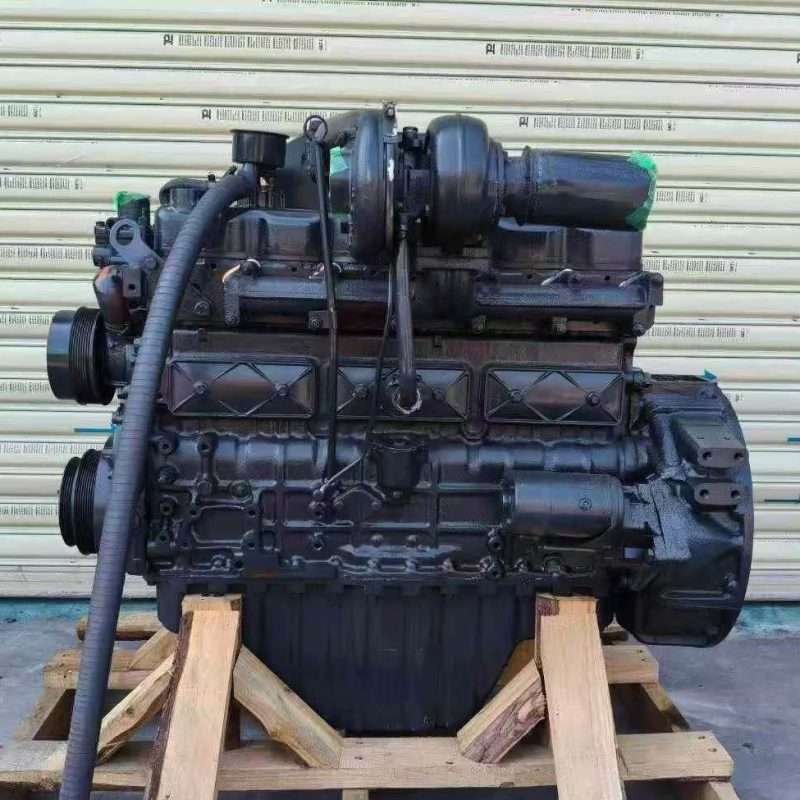
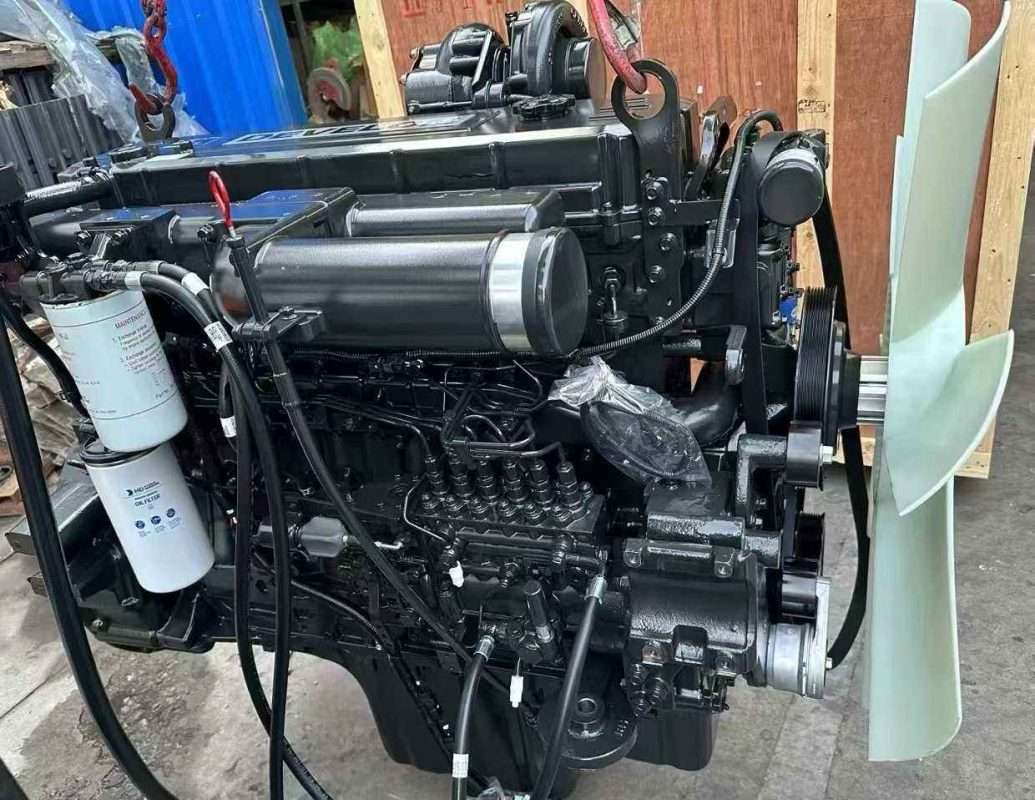
In-depth technical analysis of the Doosan DX12 engine.


In the field of heavy-duty construction machinery and large industrial power systems, the Doosan DX12 diesel engine represents the brand’s outstanding technological achievements in handling extremely high-intensity construction operations. As a power unit specifically designed for large tracked excavators ranging from 36 to 50 tons (such as the DX360LCA-7M and DX450LCA-7M) and large wheel loaders (such as the DL420A-7M), the DX12 engine utilizes the industry’s most classic and extremely durable inline six-cylinder, water-cooled, turbocharged exhaust gas engine with an air intercooler. With a total piston displacement of 11.051 liters, and thanks to its large 123 mm bore and 155 mm long stroke, this engine delivers massive power while maintaining exceptional structural compactness and overall machine operational stability. The DX12 is not merely a simple iteration of earlier models; it is a completely new power platform integrating a modern electronic power optimization system (e-EPOS) with extremely robust mechanical hardware, designed to provide uncompromising continuous high-load operation capabilities in the harshest mining and heavy earthmoving environments.
Regarding the core power output parameters of heavy-duty engineering equipment, the DX12 engine demonstrates remarkable performance benchmarks. Under continuous operation, this engine can deliver a robust effective power output of 238 to 289 kW (238 kW – 289 kW) at its rated operating speed of 1800 rpm. More importantly, its torque curve, meticulously tuned for heavy-duty conditions, allows the DX12 to instantly unleash an astonishing peak torque of 1420 to 1581 N·m within an extremely low speed range of 1200 to 1300 rpm. This signature low-speed, high-torque power output characteristic enables heavy-duty excavators weighing tens of tons to obtain a continuous source of bottom-digging force when stripping away hard rock with high resistance or digging under overload conditions. This not only avoids engine speed decay under heavy loads but also significantly reduces mechanical fatigue damage to the rear hydraulic pump and transmission system, and maximizes fuel economy.
To withstand such enormous cylinder combustion pressure and prolonged operation at extreme full load, the DX12 engine has undergone in-depth reinforcement and upgrades in the material forging and precision machining processes of its core components. Its cylinder block has undergone modern topology optimization design, resulting in a comprehensive improvement in cylinder wall thickness and overall structural rigidity. As the main shaft bearing the power, the core crankshaft assembly uses ultra-high-strength integral forged alloy steel, combined with large-sized main bearing shells and connecting rod shells, ensuring absolute resistance to bending and torsion and fatigue fracture under extreme torque output. The internal cooling water jacket of the cylinder head has also undergone a rigorous hydrodynamic redesign, enabling it to more quickly dissipate extreme heat around the combustion chamber, effectively preventing irreversible thermal deformation of the valve seats and cylinder head body under high thermal loads. At jianmingmachinery we deeply understand the crucial role these core moving components, subjected to extraordinary physical limits, play in the overall lifespan of the machine. Therefore, we are committed to providing top-tier replacement parts, including high-strength forged crankshafts, precision-machined cylinder heads, high-temperature valve components, and complete premium overhaul kits, ensuring that every DX12 engine, battling day and night in harsh mining environments, can be restored to its peak mechanical integrity after a reset.
Regarding the intake and exhaust systems and fuel delivery management, the DX12 engine is equipped with a high-efficiency exhaust turbocharger optimized for high-altitude and dusty environments, and a heavy-duty dual-filter air filtration system with a pre-filter dust collection device, which is crucial in dusty construction sites. Its turbocharger can quickly overcome turbo lag and establish positive pressure at extremely low speeds, forcing high-density fresh air into the combustion chamber for rapid and thorough mixing with the high-pressure atomized diesel fuel injected by the fuel system. To adapt to different fuel qualities worldwide, the DX12 retains an extremely reliable mechanical direct injection system architecture or a mature high-pressure fuel supply system in many demanding high-ash applications. To protect the precision fuel injection pump and multi-hole injectors, this engine also comes standard with a multi-stage fuel filter with high-precision water separation. When heavy equipment experiences power loss or abnormally increased fuel consumption due to wear of core components, timely replacement of the turbocharger assembly and precision fuel injection system components with original equipment parts is the most direct and effective way to restore the engine’s rapid throttle response and optimal intake efficiency.
The DX12 engine’s fluid management system—namely, the lubrication and cooling systems—is also an invisible mechanical shield ensuring its high-intensity continuous operation. This model is equipped with a large-capacity, deep-groove anti-tilt oil pan and a high-flow gear-driven oil pump, ensuring that high-pressure oil is stably pumped to the crankshaft main journals, connecting rod journals, and overhead valve rocker arm mechanism even when the equipment is climbing steep slopes or digging at an angle, forming a robust hydrodynamic lubricating film and completely eliminating direct metal-to-metal dry friction. A large-area plate-fin oil cooler is compactly integrated into the side of the cylinder block, strictly controlling the oil temperature within the optimal lubrication viscosity range. Regarding the cooling system, the antifreeze coolant flows evenly through the complex water passages between the cylinder liner and the cylinder head via forced circulation from a large-displacement water pump impeller. Long-term cavitation aging of the water pump impeller or excessive wear of the oil pump gears can directly lead to catastrophic consequences such as engine seizure or crankshaft failure. The OEM-grade water pump assembly, high-flow oil pump, and complete set of original factory-grade high-pressure gaskets allow the maintenance team to confidently perform in-depth preventative overhauls, completely eliminating potential catastrophic mechanical failures and ensuring a continued return on investment for heavy assets.